PETG-GF filament
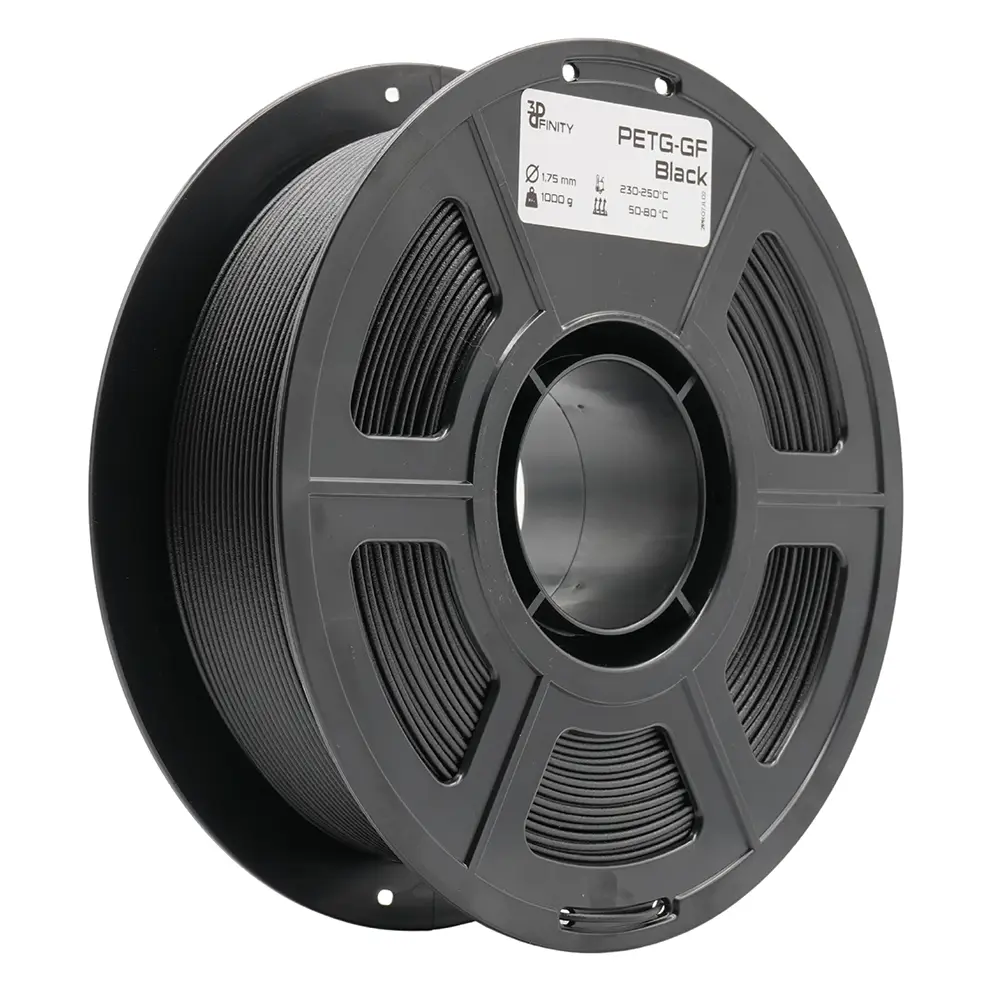
PETG-GF is PETG reinforced with glass fibre. It is intended for strong functional parts and applications where stiffness and stability matter.
Buy in E-shop →Stability and stiffness with glass fibre.
Choose PETG-GF when stiffness and stability of the functional part are the priority.
Best for
- functional technical parts
- jigs and brackets
- strong structural components
Strengths
- higher stiffness
- good part stability
- technical material character
What to consider
- abrasive material – wear-resistant nozzle recommended
- more pronounced surface texture
- requires proper drying
Advantages and limitations
Exact print settings may vary by printer, nozzle and part geometry. We'll send the technical data sheet (TDS) on request.
Advantages
- higher stiffness
- good part stability
- technical material character
Limitations
- abrasive material – wear-resistant nozzle recommended
- more pronounced surface texture
- requires proper drying
Recommended print settings for PETG-GF
Recommended values for 3DFINITY PETG-GF filament. Exact settings may vary by printer, nozzle and part geometry.
| Parameter | Recommended value |
|---|---|
| Nozzle temperature | 255–270 °C |
| Bed temperature | 75–90 °C |
| Print speed | 25–200 mm/s |
| Enclosed chamber | Not required |
| Part cooling | 0–20% from layer 3 |
| Filament drying | 65 °C / 6–10 h, recommended before printing |
| Material density | approx. 1.32 g/cm³ |
Recommended nozzle
| Nozzle | Nozzle diameter |
|---|---|
| wear-resistant | 0.6 / 0.8 mm recommended, 0.4 mm for smaller models |
Starting point setting (a first point to test)
| Nozzle | Bed | Speed | Part cooling |
|---|---|---|---|
| 260 °C | 75 °C | 80 mm/s | 0% |
Printing tips
Print dry material. A 0.4 mm nozzle is only suitable for smaller models — the fibres in the material can clog a narrower nozzle. On smooth PEI or glass, we recommend using a release layer.
These values are indicative, for a 0.20 mm layer height and a 0.4 mm nozzle (0.6 mm for CF and GF). Start with the baseline setting and fine-tune it for your printer — maximum speed can be limited by hotend flow rate. The cooling fan value in the table refers to the part-cooling fan; print the first 2 layers without cooling, overhangs and bridges may need more. Leave the hotend cooling fan at your printer manufacturer's default setting. Dry the filament in a temperature-controlled dryer, don't exceed the spool's heat resistance, and after drying store it sealed with a desiccant.
Available colours for PETG-GF filament (3DFINITY PRO)
Questions about PETG-GF
What is PETG-GF filament suitable for?
PETG-GF is PETG reinforced with glass fibre. It is intended for strong functional parts and applications where stiffness and stability matter.
Is PETG-GF suitable for outdoor use?
PETG-GF is best suited for indoor use. For parts permanently exposed to sunlight and weather, choose ASA.
What diameter and tolerance does 3DFINITY PETG-GF filament have?
PETG-GF filament is manufactured at a 1.75 mm diameter with a declared tolerance of ±0.02 mm. We make it using our own technology in Slovakia with diameter control during production.
Do I need a hardened nozzle for PETG-GF?
Yes. PETG-GF contains abrasive fibres that wear down brass nozzles. We recommend a hardened steel or otherwise wear-resistant nozzle with a diameter of at least 0.4 mm.
Need help choosing?
Compare all materials or tell us about your part's application. We'll recommend a suitable material based on environment, load and the surface finish you need.